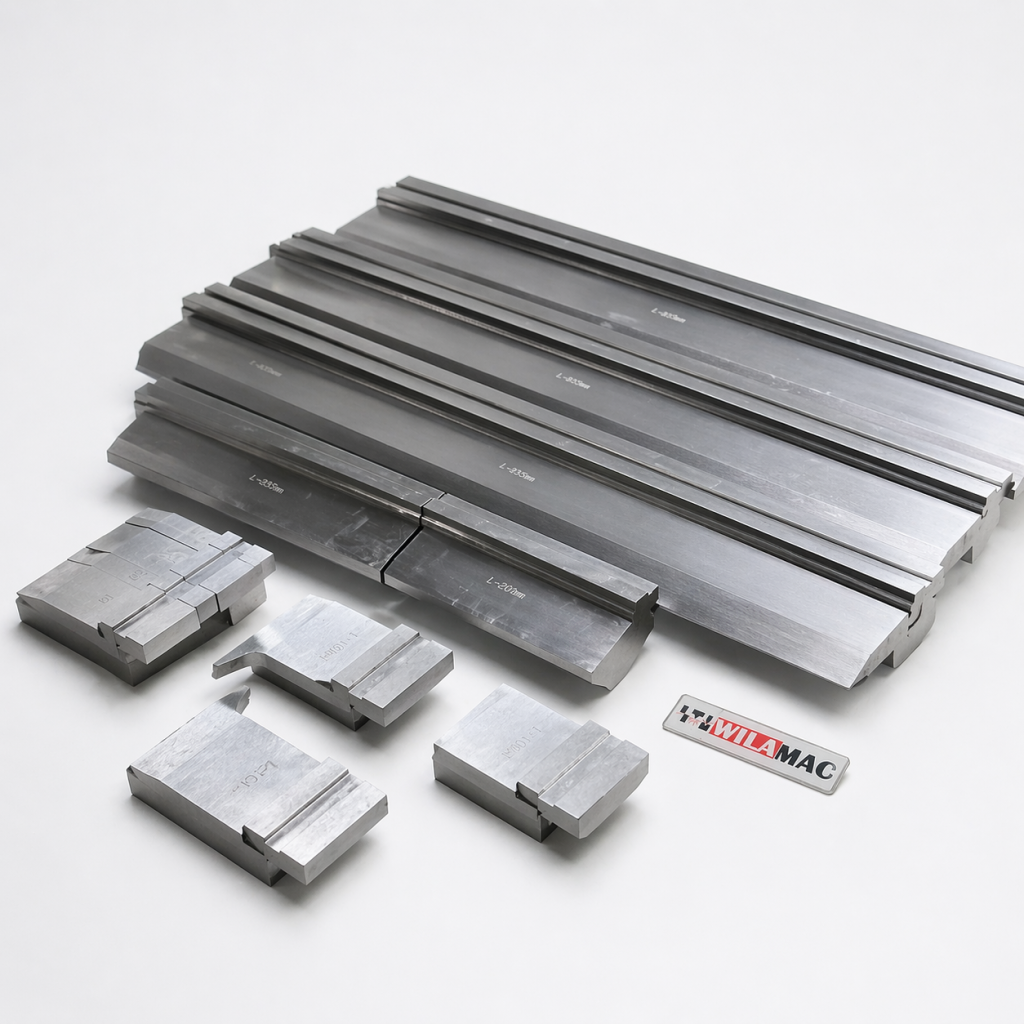

Selecting the proper press brake tooling is critical to achieving precise bend angles, avoiding costly scrap, and protecting your machine from premature wear. Whether handling standard mild steel or high-tensile stainless alloys, matching punch-and-die geometry with sheet characteristics directly determines fabrication efficiency and final part quality.
This comprehensive guide breaks down the core selection criteria, standard sizing formulas, material grades, and preventive maintenance practices for modern metal fabrication.
1. Core Selection Criteria: Material & Tonnage
Before choosing punch profiles or die openings, three foundational variables must be evaluated:
- Material Tensile Strength: High-strength materials require smaller bend radii and significantly higher bending tonnage.
- V-Opening Dimension: For mild steel under 3 mm thickness, use the standard rule:
- V = 8 * t (where t represents sheet thickness). For thicker plates or stainless steel, expand the opening to 10 * t or 12 * t to prevent surface cracking.
- Machine Load Limits: Never exceed the maximum linear load capacity (tons/meter) specified for either the punch or the die shoulder.
2. Common Tooling Types & Applications
Different workpiece profiles require specialized tool geometries to prevent collisions and maintain high throughput.
| Tooling Type | Common Applications | Key Advantages |
| Standard Punch & V-Die | 90° air bending, simple profiles, brackets | High versatility, low tooling cost, fast setup |
| Gooseneck Punch | U-channels, deep return flanges, box forming | Eliminates profile interference on interior bends |
| Acute Angle Tooling | Air bending under 60°, prep for hemming/flattening | Provides room for high springback compensation |
| Offset (Joggle) Dies | Single-stroke Z-bends and overlapping panel joints | Cuts cycle time by half compared to two-stage bends |
Tech Tip: When bending thick plates with narrow flanges, ensure the minimum flange length is at least 70% of the V-die opening width to avoid slipping.
3. Tooling Materials and Hardening Methods
Durability and dimensional stability determine your long-term cost per bend. Industrial-grade press brake tooling relies on specialized alloy chemistry and deep surface hardening:
42CrMo / AISI 4140 Alloy Steel: The global standard material providing an optimal balance of structural ductility, impact toughness, and fatigue resistance under cyclic bending forces.
Working Edge Hardness: High-frequency induction hardening applied to critical punch tips and die V-shoulders achieves 56–60 HRC to a depth of 3–4 mm, preventing premature deformation.
Anti-Galling Treatments: Nitriding or PVD coatings significantly lower surface friction, helping suppress material buildup when air-bending galvanized or soft aluminum stock.
4. Maintenance & Precision Alignment Best Practices
Routine care and correct installation protect your tooling investment and keep bend tolerances consistent across the entire bed length:
- Sectional Alignment: When installing segmented tooling, thoroughly wipe the upper clamping beam and lower tool tangs. Even minute metal filings or grit trapped behind the tang can introduce measurable angle deviations across long parts.
- Uniform Tonnage Distribution: Avoid concentrating high tonnage on very short tool segments unless the punch and die are explicitly engineered for point loading. Excessive local forces can indent the bed or deflect the upper ram.
- Cleaning and Rust Prevention: Wipe all working contact surfaces with a fine mist of anti-corrosive oil at the end of every operating shift. Store tooling vertically in dedicated cabinets with protective composite dividers to prevent accidental edge chipping.
- Routine Shoulder Inspection: Periodically examine punch tips and die shoulder radii for micro-fractures, scoring, or uneven wear, especially after high-volume runs on hot-rolled or laser-cut parts with oxide scale.
Need Custom Press Brake Tooling or Bending Calculations?
Submit your CAD drawings, material specifications, and machine model to our engineering team for a full bending feasibility analysis and fast quotation.
[ Request a Custom Tooling Quote ]