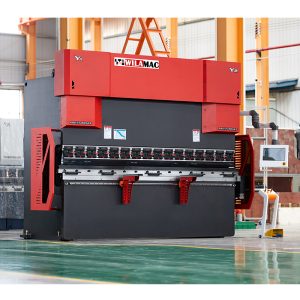

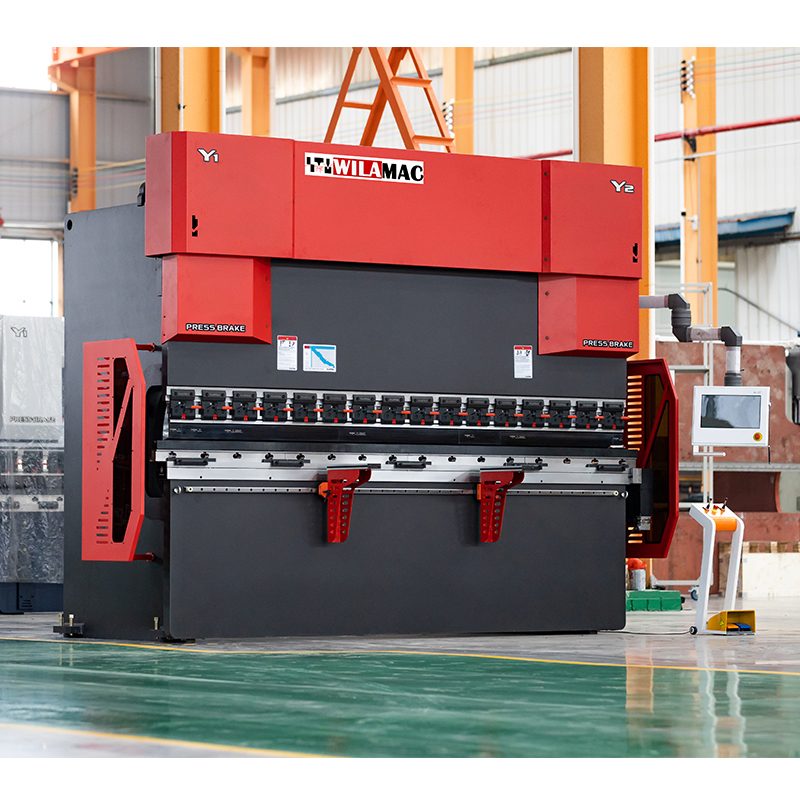
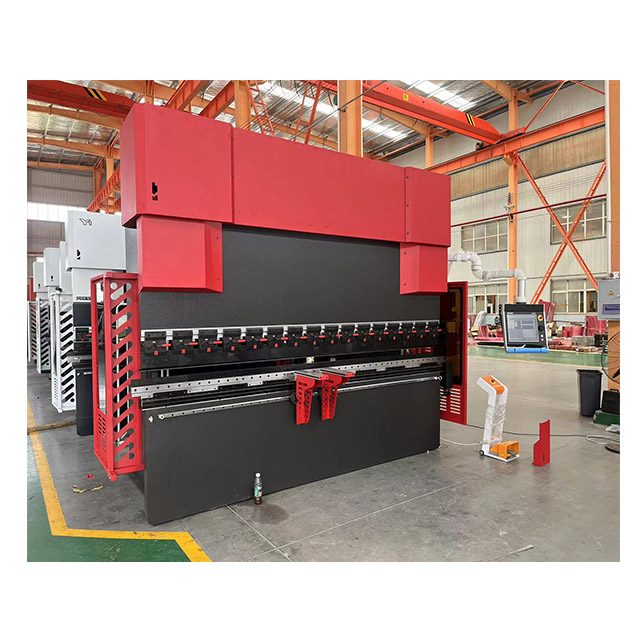
400T / 3200mm CNC Press Brake — 6+1 Axis with DELEM DA-69T Control
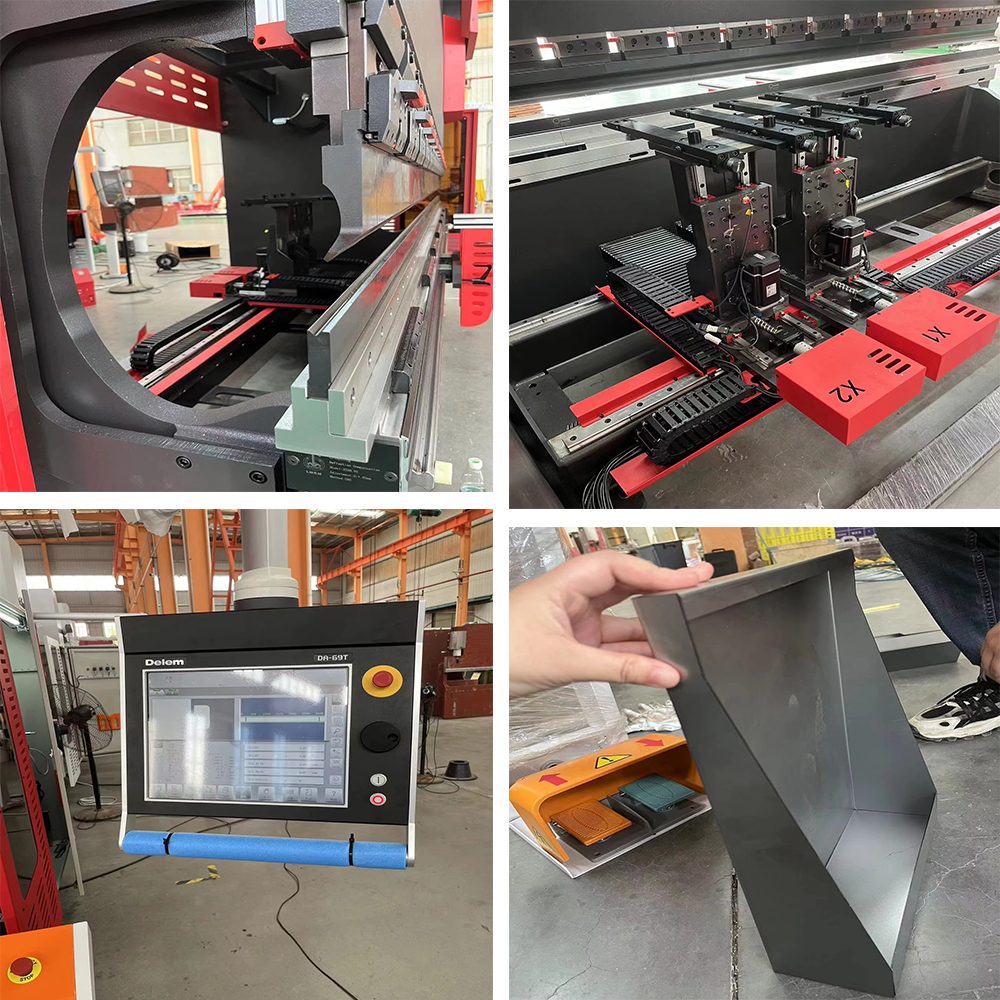
400 tonne CNC hydraulic press brake with a 3200mm working table, a 6+1 axis configuration and DELEM DA-69T control. Electro-hydraulic servo drive with a fully automatic bending cycle — backgauge position, ram depth and bend sequence come off the control rather than off the operator, so the same part repeats at the end of a shift as it did at the start. The tonnage and the 3200mm length together are what let you form heavy gauge over the full bed without the bend opening up in the middle. Send us your thickest and longest part, the material grade and the inside radius, and we will confirm the crowning and the axis configuration before quoting.
| Machine Type | CNC hydraulic press brake |
|---|---|
| Nominal Capacity | 400 T |
| Working Table Length | 3200 mm |
| Slider Stroke | 200 mm |
| Throat Depth | 400 mm |
| Drive | Hydraulic |
| Axis Configuration | 6+1 axis |
| Control System | DELEM DA-69T |
| Cycle | Fully automatic |
| Machinery Test Report | Provided |
| Video Outgoing-Inspection | Provided |
| After-sales Service | Engineers available to service machinery overseas |
| Place of Origin | China |
| Brand | WILAMAC |
| Minimum Order Quantity | 1 |
What a 400T CNC Press Brake Is Built For
A 400 ton press brake is the size of machine you buy when the parts get thick and long at the same time. The tonnage is what lets you form heavy gauge over a full 3200mm length without the beam deflecting and the bend opening up in the middle.
The tonnage figure only means something alongside the table length. A machine rated at 400 tonnes over 3200mm carries a different load case from the same tonnage on a shorter bed, and the crowning system has to suit the width of work you actually bend. If most of your parts sit at one end of the table, you are paying for capacity you are not using; if they run the full length, the crowning and the beam stiffness are what keep the angle consistent from one end to the other.
This machine runs a 6+1 axis configuration with a DELEM DA-69T control and an electro-hydraulic servo drive, with the bending cycle fully automatic. In practice that means the backgauge position, the ram depth and the bend sequence come off the control rather than off an operator’s judgement, which is what makes the same part repeat at the end of a shift as it did at the start.
Specifying a 6+1 Axis CNC Press Brake
Start with the part, not the tonnage chart. Send us the thickest and the longest part you intend to bend, the material grade, and the inside radius you need. Material grade matters because high-tensile and stainless sheet need more force for the same thickness, so a machine sized on mild steel alone will come up short the first time you run a harder grade.
Then tell us what the control has to do. Axis count follows the work: more axes mean more backgauge movement set from the program instead of by hand, which pays back on anything with a repeated sequence of different bends.
What to send us:
- Thickest and longest part, material grade, and required inside radius
- Bend sequence and how many different bends per part
- Whether the backgauge has to move between bends on its own
- Control and axis configuration you need, and the tooling system you already run
- Voltage and phase at your site
Send us those and we will confirm the tonnage, the axis configuration and the crowning before quoting.
Related Products


